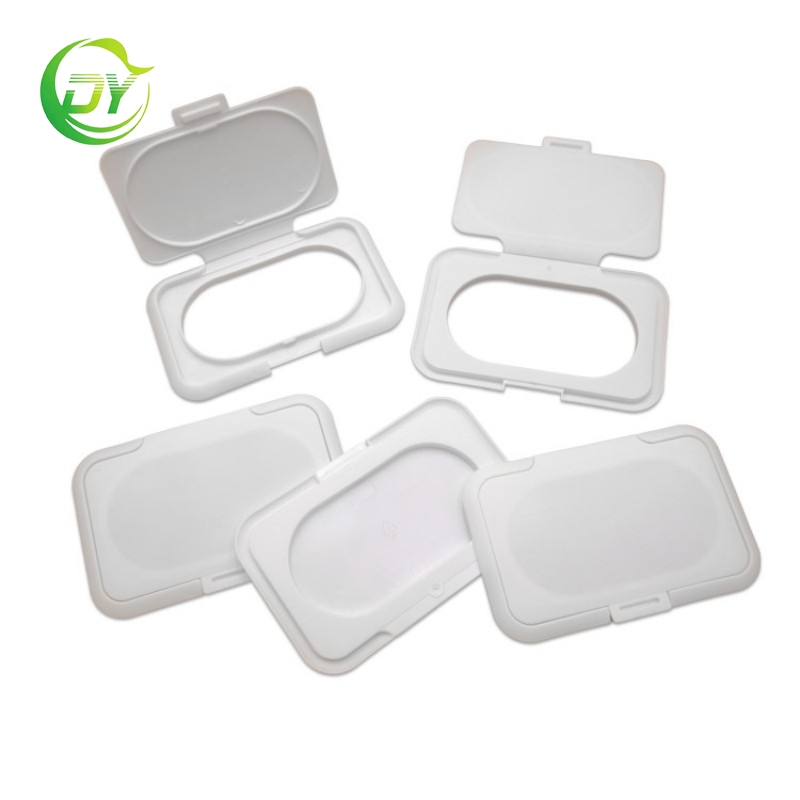
Plastic Wet Wipes Lid Wholesale buyers need lids that open smoothly, close tightly, and protect the wipes from drying out. However, poor mold design or unstable injection molding can cause leaks, weak hinges, rough edges, and poor appearance. Common defects include sink marks, weld lines, and short shots.
These defects can increase rejection rates and slow down filling and packing lines. They may also reduce the shelf life of wet wipes. A lid with a 0.5 mm gap around the sealing edge can allow moisture loss during storage.
This guide explains the main injection molding defects in plastic wet wipes lids and shows how a wet wipes lid manufacturer can prevent them through mold design, process control, and inspection. It also covers plastic lid quality control, polypropylene lid molding, and high speed injection molding.
The most common injection molding defects in plastic wet wipes lids are flash, short shots, sink marks, weld lines, warpage, burn marks, flow marks, gate blush, and dimensional variation. The main causes are poor mold venting, incorrect melt temperature, unstable injection pressure, uneven cooling, excessive shrinkage, and improper material drying. A reliable solution combines mold flow analysis, balanced gate design, controlled cooling, regular machine calibration, and inspection based on standards such as ISO 2859-1 and ISO 20457.
Flash is a thin layer of extra plastic that forms along the parting line, hinge, latch, or sealing edge. It often feels sharp when touched. Flash may prevent the lid from closing fully or create a poor appearance.
| Control item | Recommended check | Reason |
|---|---|---|
| Flash height | Keep below 0.05 mm on the sealing edge | Protects closure and sealing performance |
| Parting line gap | Keep within the approved mold drawing tolerance | Reduces plastic leakage during molding |
| Clamping force | Set according to projected area and process validation | Prevents mold opening during injection |
| Visual inspection | Inspect 100 percent of the first 5 shots after a mold change | Finds early process problems |
A short shot occurs when the cavity does not fill completely. The defect may appear at the hinge, latch, corners, thin ribs, or outer rim. A short shot can make the lid weak and may stop the snap closure from working.
Use mold flow analysis before steel cutting. The analysis should check filling time, pressure loss, weld line location, and air traps. For a multi-cavity mold, filling time between cavities should normally be kept within a narrow validated range. A difference of more than 5 percent should trigger a process review.
For polypropylene wet wipes lids, the process engineer should also check melt temperature, injection speed, cushion size, and gate freeze time. These values must be confirmed through a documented trial instead of copied from another lid design.
Sink marks are shallow depressions on the outer surface. They often appear above thick ribs, bosses, hinge supports, or latch structures. Internal voids are empty spaces inside the part. Both defects are linked to uneven cooling and plastic shrinkage.
| Design area | Practical target | Quality risk if ignored |
|---|---|---|
| Main wall | Use a uniform wall based on the product drawing | Uneven shrinkage and surface dents |
| Rib thickness | Usually keep near 40 to 60 percent of the main wall thickness | Visible sink marks |
| Cooling balance | Keep cavity temperature variation within the validated range | Warpage and dimensional changes |
| Holding stage | Continue until the gate is frozen | Incomplete packing and voids |
Weld lines appear where two plastic flow fronts meet. They may look like thin lines, color changes, or small grooves. On a wet wipes lid, weld lines often form near the hinge, latch, label area, and holes.
A visible weld line is not always a failure. However, a weld line located on a living hinge or snap hook can reduce strength. Repeated opening and closing may cause cracking.
As a practical validation target, a lid design can be tested for at least 500 opening and closing cycles. The hinge should not show cracks, separation, or loss of function after testing. The final cycle count should match the customer's use requirement.
Warpage occurs when different areas of the lid shrink at different rates. The lid may twist, bow, or lift at the corners. Dimensional variation can also cause poor fit between the lid and the wet wipes container.
| Inspection item | Suggested method | Example acceptance control |
|---|---|---|
| Overall length and width | Digital caliper or coordinate measuring machine | Use the approved drawing tolerance |
| Flatness | Granite surface plate and height gauge | Set a product specific limit, such as 0.5 mm |
| Closure fit | Assembly test with the matching container | No lifting at the four corners |
| Leak or moisture protection | Closure and storage test | No visible opening or loss of seal after validation |
Burn marks are dark brown or black areas caused by compressed air or gas. They often appear at the end of the filling path, near deep ribs, or around the hinge.
When air cannot escape, the advancing plastic compresses it. The temperature of the compressed air rises quickly. This can burn the resin and damage the mold surface.
For stable production, record vent cleaning after a defined number of shots. A common starting point is every 50,000 to 100,000 shots, followed by adjustment based on actual contamination and defect data.
Flow marks appear as lines or rings that follow the movement of the plastic. Jetting creates a snake-like line near the gate. Gate blush is a cloudy or stressed area around the gate location.
| Defect | Likely cause | Corrective action |
|---|---|---|
| Flow marks | Unstable flow front or uneven cooling | Adjust injection speed and mold temperature |
| Jetting | Plastic enters the cavity too fast without contacting the wall | Use a slower initial speed and improve gate direction |
| Gate blush | High shear stress near a small gate | Review gate size, speed, and melt temperature |
| Color streaks | Poor mixing, contamination, or incorrect color masterbatch | Clean the barrel and confirm material dosing accuracy |
Cracks may form during ejection, assembly, transport, or repeated opening. They often start at sharp corners, ejector marks, weld lines, or thin hinge sections.
For each production lot, retain samples for traceability. A practical control plan may include 5 samples per cavity for appearance, dimensions, closure force, and hinge function. Record the mold number, cavity number, resin lot, machine number, and production time.
Plastic shrinkage changes the final size of the lid after cooling. The exact value depends on resin grade, wall thickness, mold temperature, holding pressure, and cooling time. The mold designer must use the resin supplier data and confirm the value through trial production.
Ejection marks appear as white spots, dents, or raised circles. Part sticking can bend the lid or damage the hinge. These problems may result from insufficient draft, excessive mold polish, poor ejection balance, or an overly hot part.
| Control point | Recommended practice |
|---|---|
| Draft angle | Use a suitable draft based on surface texture and mold design |
| Ejector layout | Distribute pins around strong structural areas |
| Demolding temperature | Remove the part only after enough cooling and stiffness |
| Mold release | Do not depend on release agent to solve poor mold design |
Inspectors should check flash, short shots, sink marks, weld lines, burn marks, flow marks, color variation, scratches, contamination, and deformation. Use a defined light source and viewing distance. A simple internal standard may require inspection at 30 cm under 600 to 1,000 lux lighting.
Use ISO 2859-1 as a reference for lot sampling. The exact inspection level and acceptance quality limit must be agreed with the buyer. Use ISO 20457 as a reference for tolerances and quality requirements for molded plastic parts. Calipers, gauges, torque testers, force gauges, and coordinate measuring machines should have valid calibration records.
| Inspection stage | Typical inspection content | Record required |
|---|---|---|
| First article | Full dimensions, material, appearance, and function | First article report | In-process inspection | Appearance, weight, closure, and key dimensions | Hourly or batch inspection record |
| Final inspection | Sampling based on the approved quality plan | Final inspection report |
| Pre-shipment review | Quantity, packing, labels, and product identification | Shipment release record |
A qualified plastic lid program should include a documented mold design review, at least one formal mold trial, a corrective action record for each major defect, and a production validation run. Buyers can request data from 3 consecutive production lots. The data should show stable weight, dimensions, appearance, and closure performance.
For a Dongyang sourcing project, buyers should confirm factory capacity, mold maintenance plans, inspection equipment, and export packing controls. A supplier that reports cycle time, cavity output, rejection rate, and corrective action results gives buyers a clearer basis for comparison than a supplier that only provides a unit price.
| Defect | Visible symptom | Most likely cause | First corrective action |
|---|---|---|---|
| Flash | Thin extra plastic at the edge | Mold gap or excessive pressure | Check parting line and clamping force |
| Short shot | Incomplete lid or missing rib | Low flow or trapped air | Check gate, venting, pressure, and speed |
| Sink mark | Depression above a rib | Thick section and poor packing | Review rib thickness and holding pressure |
| Weld line | Line where flow fronts meet | Multiple flow paths or low temperature | Review gate position and venting |
| Warpage | Twisted or bowed lid | Uneven cooling or shrinkage | Balance cooling and holding conditions |
| Burn mark | Brown or black area | Compressed trapped air | Clean or improve mold vents |
| Gate blush | Cloudy area near gate | High shear stress | Adjust gate design and initial speed |
| Crack | Break near hinge or latch | Stress, poor ejection, or weak weld line | Check material, ejection, and hinge design |
Common injection molding defects in plastic wet wipes lids include flash, short shots, sink marks, weld lines, warpage, burn marks, flow marks, gate blush, cracks, and dimensional variation. Most defects can be reduced through correct mold design, balanced cooling, suitable injection settings, effective venting, and documented inspection.
For Plastic Wet Wipes Lid Wholesale projects, buyers should review more than price. They should compare material control, mold capability, cycle time, inspection equipment, traceability, and long-term hinge performance. A supplier that uses measured data and a clear quality plan can deliver plastic wet wipes lids with better fit, appearance, and moisture protection.