Poor lid bonding can cause leaks, drying wipes, open packs, and costly customer complaints. Wet wipes lid bonding depends on surface energy, corona treatment, and peel strength. These three factors affect whether a plastic lid stays attached to the pack during filling, transport, and use.
The most common failures occur when the packaging film is contaminated, the adhesive does not match the film, or the application pressure is too low. A stable bonding process must control the film type, adhesive layer, bonding temperature, pressure, and storage time.
This guide explains the main causes of poor adhesion to packaging film and gives a practical inspection method for manufacturers, importers, and distributors. Dongyang produces plastic wet wipes lids for different flexible packaging structures and can help buyers select a suitable bonding method.
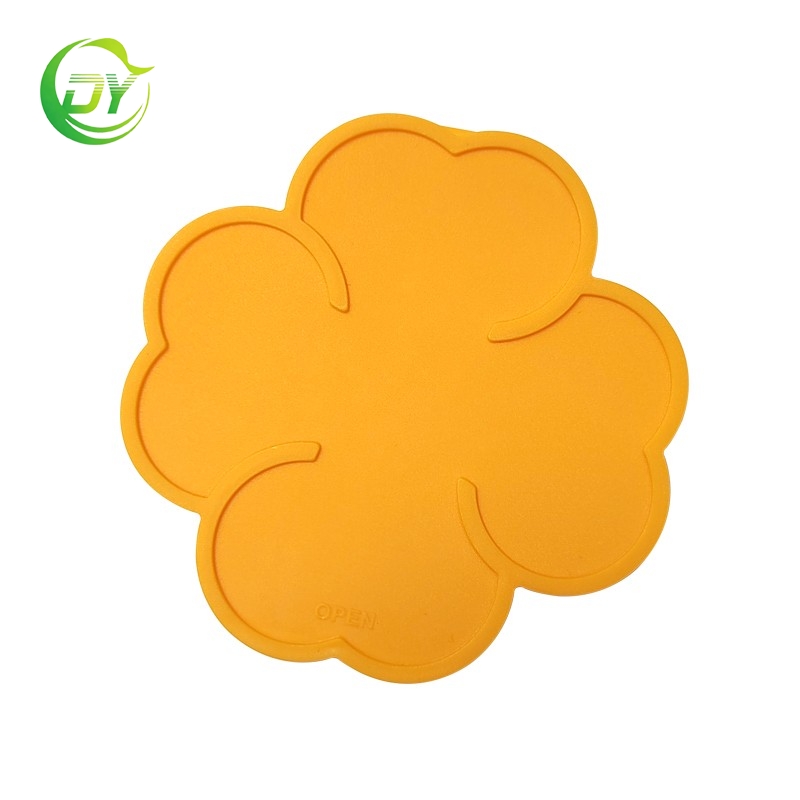
Poor adhesion means the lid does not remain firmly attached to the wet wipes package. The failure may appear during production, after storage, or when the consumer opens and closes the lid.
| Visible problem | Likely meaning | Quality risk |
|---|---|---|
| One corner lifts | Low pressure or curved film | Progressive edge peeling |
| Full lid separates | Adhesive and film are not compatible | Pack cannot be sealed correctly |
| Adhesive remains on the lid | Weak contact with the film | Low peel strength |
| Film tears during testing | Bond is stronger than the film | Possible good adhesion, but poor film strength |
| Bond is strong at first but fails later | Moisture, aging, or adhesive migration | Returns after transportation |
A lid can look bonded while still having low peel strength. Testing only by touch is not enough. A useful quality program checks the peel force, the failure pattern, and the bond after storage at different temperatures and humidity levels.
Polyethylene and polypropylene films often have low surface energy. This makes them difficult for many adhesives to wet and spread across. If the adhesive forms small gaps instead of a continuous layer, the lid may peel from the edge.
Many flexible films use a surface treatment to improve bonding. Corona treatment is common, but its effect can reduce over time. A film that bonded well when produced may become harder to bond after weeks of storage.
Check: Test the film surface with dyne pens or another approved surface energy method. A starting target of about 38 to 42 dynes per centimeter is often used for treated polyolefin film, but the correct value depends on the adhesive and film structure.
Even a small amount of contamination can create a weak boundary between the lid adhesive and the packaging film. Common contaminants include dust, printing ink, silicone, machine oil, hand lotion, and residue from wet wipe liquid.
Contamination can enter during film rewinding, lid feeding, manual handling, or filling. It may also spread from a roller or conveyor to many packages in a short time.
Check: Compare bonding on a clean film sample with bonding on a production sample. If the clean sample performs well, inspect film handling, gloves, rollers, work tables, and filling equipment.
A pressure sensitive adhesive may work well on one film but poorly on another. The film may contain polyethylene, polypropylene, polyester, metallized layers, or a laminate. Each layer can affect wetting, flexibility, and long-term adhesion.
Wet wipe liquid also matters. Alcohol, oil, fragrance, preservatives, and surfactants may contact the lid area or migrate through the package. Some liquids reduce adhesive tack or soften the adhesive after storage.
Check: Test the lid on the exact production film with the exact wet wipe formulation. Do not approve a lid only from a dry laboratory sample.
Pressure sensitive adhesive needs close contact with the film. If the applicator does not press the lid evenly, air pockets and unbonded areas can remain under the adhesive. A rigid lid may also bridge over wrinkles or uneven film.
Low pressure can result from a worn roller, incorrect machine height, poor lid placement, high line speed, or a film surface that is not flat. The problem often appears as lifting at the front or rear edge.
Check: Inspect the complete contact area immediately after application. Reduce the line speed for a trial and increase controlled pressure in small steps. Record each setting instead of changing several factors at once.
Some lid systems use pressure sensitive adhesive, while others use heat seal coatings or a combination of materials. A heat seal system may need a controlled temperature, dwell time, and pressure window. Too little heat can create a weak seal. Too much heat can damage the film or adhesive.
Temperature can also change the flexibility of the film. A film that becomes soft may wrinkle under the lid. A film that becomes too rigid may resist contact with the adhesive.
Check: Record the actual temperature at the bonding surface, not only the machine display. Start trials within the supplier's recommended range and adjust one setting at a time.
Some adhesives need time to build final peel strength. If the pack is boxed, stacked, or exposed to heavy handling immediately after lid application, the bond may be disturbed before it becomes stable.
Heat seal coatings also need enough dwell time to form a continuous seal. High production speed can reduce contact time below the process requirement.
Check: Test samples after 10 minutes, 24 hours, and 72 hours. A large increase in peel strength can show that the process needs a longer conditioning period.
A lid must match the flat bonding area of the package. If the lid is too small, the adhesive margin may be narrow. If it is too large, the edge may bend or catch during transport. A curved or flexible lid may not provide equal pressure across the entire surface.
Wrinkles are another common cause. A wrinkle under the lid creates a channel where air and moisture can enter. The problem may be caused by excessive film tension, uneven filling, or an unsuitable package shape.
Check: Confirm lid length, width, adhesive border, opening position, and package flatness. A practical design review should measure at least 10 packs from different areas of the production run.
| Film structure | Typical bonding concern | Recommended evaluation |
|---|---|---|
| Polyethylene film | Low surface energy and treatment decay | Check dyne level, cleaning, and adhesive wetting |
| Polypropylene film | Low polarity and possible film additives | Run compatibility and aging tests |
| Polyester laminate | Different surface layers and higher stiffness | Bond to the actual outer layer, not the inner layer |
| Metallized laminate | Surface variation and flex cracking | Test after folding, rubbing, and temperature cycling |
| Printed film | Ink, varnish, and coating contamination | Place the lid on the approved bonding zone |
The adhesive bonds to the surface that it touches. A laminate may contain several layers, but only the outer bonding layer controls the first contact. Always provide the lid supplier with the complete film specification and a real production film sample.
Use the following process when a wet wipes lid fails an adhesion test. It helps separate material problems from machine problems.
Flow: Failed pack inspection, surface and material check, machine setting trial, peel test, aging confirmation, final approval.
Take samples at the beginning, middle, and end of a production run. A basic check can use 10 packs from each point. For a larger validation, compare at least three film lots and three lid lots. This can reveal roll-to-roll or batch-to-batch variation.
Peel testing is more useful than a simple visual check. The test should use a fixed peel angle, speed, sample width, and conditioning time. Record whether the failure occurs at the adhesive interface, inside the adhesive, or in the film.
| Test stage | What to record | Purpose |
|---|---|---|
| Immediate test | Initial peel force and visible gaps | Checks application quality |
| 24-hour test | Peel force and failure mode | Checks bond development |
| 72-hour test | Final stable adhesion | Checks short-term aging |
| Humidity test | Peel force after exposure | Checks moisture resistance |
| Temperature cycle | Edge lifting and film damage | Checks transport conditions |
There is no single peel strength value for every wet wipes pack. The correct target depends on film strength, lid opening force, consumer use, package size, and adhesive type. A good specification must balance secure bonding with easy opening.
If the bond is too weak, the lid lifts during shipping. If it is too strong, the consumer may tear the film or struggle to open the pack. Test both lid attachment and repeated opening and closing. The package should remain closed after use without becoming difficult to operate.
Start with the lowest-risk correction. Clean the bonding area, improve film handling, and confirm the lid position before changing the adhesive. A material change can create new problems with opening force, recyclability, cost, or product appearance.
Buyers should provide suppliers with the film type, film thickness, adhesive location, wet wipe ingredients, filling speed, storage temperature, and expected shelf life. These details help a lid manufacturer recommend a more reliable bonding structure.
Dongyang supplies plastic wet wipes lids for overseas buyers, distributors, and packaging manufacturers. Lid selection can be reviewed according to pack size, opening shape, flexible film structure, adhesive type, and production speed.
For a new project, buyers should request a sample trial using the actual packaging film. The trial should include immediate adhesion, 24-hour adhesion, storage testing, and repeated lid opening. This approach is more reliable than selecting a lid from appearance alone.
A supplier should also confirm lid dimensions, adhesive coverage, material information, color, packaging method, and inspection standards. Clear specifications reduce the risk of receiving lids that look correct but perform poorly on the production line.
The adhesive may lose strength because of moisture, heat, wet wipe liquid, or chemical migration. The film surface may also have low treatment stability. Test the pack after 24 hours, 72 hours, and the expected storage period.
No. Higher pressure cannot fully correct contamination, an unsuitable adhesive, low surface energy, or a wrinkled film. Pressure should be adjusted only after the materials and bonding area are confirmed.
Send the film structure, thickness, surface treatment, printing position, wet wipe formula, pack dimensions, production speed, storage conditions, and target opening force. A real film sample is also strongly recommended.
Poor adhesion to packaging film usually comes from seven areas: surface energy, contamination, adhesive compatibility, pressure, temperature, dwell time, and package design. The fastest route to a solution is to inspect the failure pattern, measure the film surface, control the machine settings, and confirm performance through peel and aging tests.
When these controls are included before mass production, manufacturers can reduce lid lifting, leakage, drying wipes, and customer complaints. Dongyang can support plastic wet wipes lid selection and sample testing for different flexible packaging films and overseas markets.