Choosing a wet wipes lid is not only a matter of lid size. Packaging film compatibility, adhesive peel strength, and heat seal performance all affect whether a lid stays attached and protects the wipes. For overseas buyers, the most important question is simple: which film works best with a plastic wet wipes lid?
PE packaging film is flexible and widely used, but its low surface energy can make adhesive bonding difficult. PET packaging film is stronger and more stable during production. Laminated packaging film can provide the best barrier, but its outer layer, coating, ink, and adhesive system decide the final result.
The practical conclusion is clear. PET usually gives the most predictable lid bonding. PE can work well when the surface is treated and the correct adhesive is selected. Laminated films require a complete packaging test because the same lid may perform differently on two laminate structures.
Quick answer: A compatible wet wipes lid must match the film surface, adhesive, opening size, production speed, and storage conditions. A lid that passes a hand test may still fail after 30 days of storage or transport.
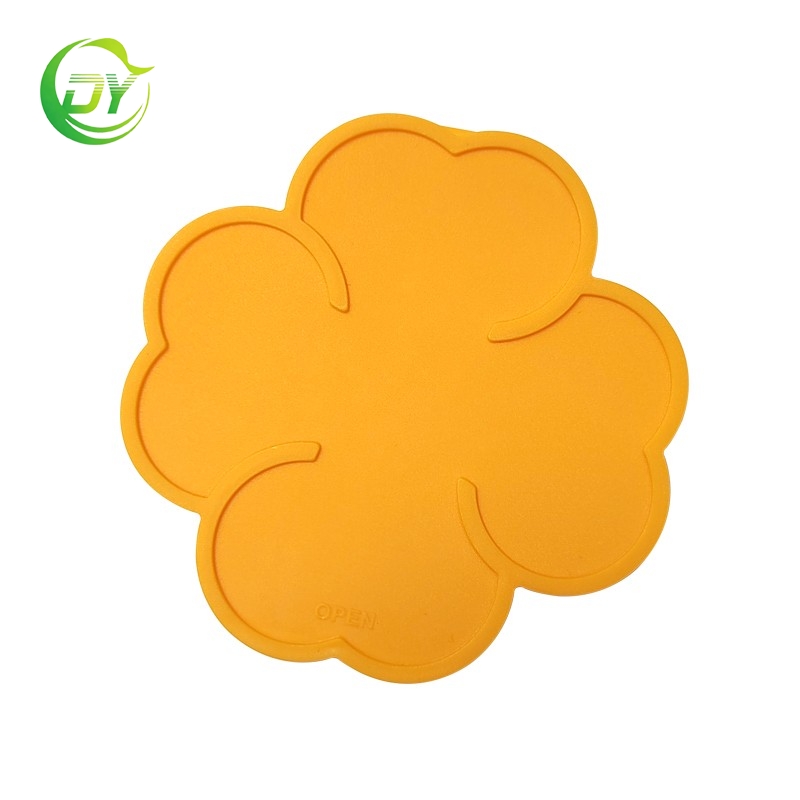
1. What Determines Wet Wipes Lid Compatibility?
Compatibility means that the lid remains firmly attached, opens smoothly, closes repeatedly, and protects the moisture inside the pack. It also means that the film does not tear, stretch, curl, or lose its printed finish around the lid.
A complete compatibility decision has five parts: film type, film thickness, surface treatment, lid material, and attachment method. The adhesive or heat seal layer is also important. Ignoring one part can create leakage, lifting corners, or a lid that cannot be opened by the final user.
The main technical factors
- Surface energy: Low-energy PE is harder to bond than PET.
- Film flexibility: A soft film can pull against the lid during pouch movement.
- Film thickness: Thin films may wrinkle under the lid flange.
- Surface finish: Ink, varnish, matte coating, and anti-slip treatment can reduce bonding.
- Opening design: The lid must cover the opening without blocking wipe removal.
- Storage conditions: Heat, humidity, alcohol, lotion, and transport vibration can change results.
A lid is part of a packaging system
A plastic lid may be made from PP or another rigid plastic. The lid body can be suitable for the product, while the attachment system is not suitable for the film. For this reason, buyers should test the complete combination instead of approving the lid alone.
Dongyang supports buyers by checking lid size, flange design, adhesive selection, and packing conditions before mass production. A proper sample review can prevent thousands of finished packs from needing rework.
2. PE Packaging Film: Flexible and Cost Efficient, but More Difficult to Bond
PE, or polyethylene, is common in wet wipes packaging because it is flexible, light, and resistant to water. It is also suitable for high-speed pouch production. However, untreated PE has a low surface energy. Many common pressure-sensitive adhesives do not spread evenly on it.
This can lead to low initial tack, lifting corners, and poor peel strength. The problem may become worse when the pack contains lotion or when the film is stored in a hot warehouse. PE also moves more than PET when the pouch is squeezed or folded.
How to improve PE lid bonding
- Confirm whether the PE surface has corona treatment.
- Check the treatment level after printing and pouch making.
- Use an adhesive designed for low-surface-energy plastics.
- Keep the film clean and free from oil, dust, and lotion.
- Apply enough pressure during lid attachment.
- Test the pack after heat aging and cold storage.
Corona treatment can improve the surface for printing and bonding, but its effect may reduce with time. A film that tested well at the factory may show weaker bonding after several months. Buyers should ask the film supplier for treatment information and test the actual production roll.
Typical PE test starting points
For development, many packaging teams begin with a 24-hour peel test and then compare results after heat aging at about 40 to 50 degrees Celsius. A useful internal target may be 1.0 to 2.0 N per 25 mm, but the correct value depends on the lid size, film structure, and customer standard.
These figures are development references, not universal product specifications. The final target should be agreed with the buyer and tested on the actual PE film, actual lid, and actual wet wipe formula.
3. PET Packaging Film: More Stable for Lid Attachment
PET, or polyethylene terephthalate, has higher stiffness and better dimensional stability than PE. This helps the film stay flat under the lid flange. PET is often used as an outer layer in flexible packaging because it supports printing, handling, and barrier structures.
In many cases, PET offers a more consistent bonding surface. It is less likely than PE to stretch away from the lid when the pouch is opened. This can improve the appearance of the pack and reduce corner lifting during distribution.
Important PET limitations
PET is not automatically compatible with every lid. A coating, printed varnish, or laminate adhesive may be located between the lid adhesive and the PET layer. If the lid bonds to a weak coating instead of the film, the surface may separate during peeling.
PET is also stiffer. If the pouch design uses a very flexible opening area, the film may crease near the flange. A well-designed lid flange and suitable adhesive thickness can reduce this risk.
When PET is a good choice
- When the package needs better dimensional stability.
- When a clean printed surface is important.
- When the lid must be opened and closed many times.
- When high-speed packing creates film movement.
- When the buyer wants a more consistent peel result.
For a premium wet wipes pack, PET can provide a firm and neat base for a plastic wet wipes lid. The best result still depends on the outer coating and the adhesive selected by the converter.
4. Laminated Packaging Film: Judge the Outer Layer, Not Just the Name
Laminated packaging film may contain two or more layers, such as PET/PE, PET/CPP, BOPP/PE, or other structures. Lamination improves barrier protection, stiffness, print quality, and sealing. However, the lid does not bond to every layer. It bonds only to the surface that touches the lid adhesive.
For example, a PET/PE structure may have PET on the outside and PE on the inside. If the lid is applied to the PET side, it may show different peel behavior than a pack using a PE outer surface. The film name alone is not enough for approval.
Questions buyers should ask about laminates
- Which layer is the outer lid attachment surface?
- Is the surface printed, coated, or varnished?
- What is the total film thickness?
- Is there a slip agent or anti-block additive?
- Can the outer layer withstand repeated peeling?
- Will the laminate curl after cutting or heat exposure?
The weak point may be the film surface, the ink layer, the lamination bond, or the lid adhesive. A peel test should record the failure mode. A clean adhesive separation is different from film tearing, ink removal, or coating delamination.
5. PE, PET and Laminated Film Comparison
| Film type | Main advantages | Main lid bonding risk | Recommended control | General suitability |
|---|---|---|---|---|
| PE | Flexible, light, water resistant, cost efficient | Low surface energy and film stretching | Surface treatment, low-energy adhesive, pressure control | Good after validation |
| PET | Stable, stiff, printable, less film movement | Coating or ink may become the weak layer | Check coating, flange design, and peel failure mode | Usually the most predictable |
| Laminated film | Strong barrier, good appearance, flexible structure choices | Different outer layers and delamination risk | Test the complete laminate and printed surface | Good when structure is confirmed |
The table gives a general comparison. It does not replace a production trial. A high-quality PET laminate can fail if its outer varnish is not suitable. A treated PE film can perform better than an untreated PET-coated film.
6. Adhesive and Attachment Method Selection
Most plastic wet wipes lids are attached with a pressure-sensitive adhesive, a hot melt adhesive, or another adhesive system. Some packaging designs use a heat seal layer or a pre-applied seal around the opening. The right method depends on the lid flange, film surface, machine speed, and required opening force.
Pressure-sensitive adhesive
Pressure-sensitive adhesive is convenient for many plastic lids. It bonds when pressure is applied and can support a resealable lid design. It must be selected for the actual film surface. Low-energy PE may need a special adhesive, primer, or surface treatment.
Heat seal attachment
Heat sealing can provide a strong bond when the film includes a compatible sealant layer. Temperature, pressure, and dwell time must be controlled. Too much heat may deform the lid or damage the film. Too little heat may create channels and leakage.
Opening force and resealing
A strong lid is not always a good lid. If the opening force is too high, the consumer may struggle to open it. If the force is too low, the lid may open during transport. A practical development range can be established by testing at least 10 samples before and after aging.
7. Step-by-Step Compatibility Testing Flow
Use the following process before placing a large wholesale order. It helps buyers compare lids on the same film and prevents decisions based only on appearance.
- Identify the film: Record PE, PET, or the full laminate structure.
- Record the film data: Measure thickness, surface treatment, coating, and printed area.
- Select the lid: Confirm lid dimensions, flange width, material, and closure design.
- Prepare samples: Use the actual wet wipe liquid, pouch shape, and production film.
- Apply the lid: Keep pressure, temperature, and application speed consistent.
- Check initial bonding: Inspect corners, wrinkles, bubbles, and adhesive coverage.
- Run peel tests: Test at 180 degrees where possible and record the failure mode.
- Run aging tests: Store samples at room temperature and at about 40 to 50 degrees Celsius.
- Test repeated opening: Open and close each lid 10 to 20 times.
- Approve the system: Confirm film, lid, adhesive, machine settings, and storage limits.
Flow summary: Film identification to surface inspection to lid selection to sample application to initial peel test to aging test to repeated opening test to production approval.
Recommended sample quantities
For an early comparison, test at least 10 packs for each film and lid combination. For a production approval, use samples from different rolls and production times. This helps reveal variation caused by film treatment, adhesive coating, machine pressure, and operator handling.
8. Common Problems and Practical Solutions
| Problem | Likely cause | Practical solution |
|---|---|---|
| Lid corners lift | Low surface energy, low pressure, or narrow flange | Use a suitable adhesive and increase controlled application pressure |
| Film tears during opening | Adhesion is stronger than the film or the film is too thin | Reduce opening force and review film thickness |
| Ink comes off with the lid | The lid bonds to a weak ink or varnish layer | Change the printed surface or use a compatible coating |
| Lid opens during transport | Low tack, poor pressure, or contamination | Clean the surface and check adhesive coverage and storage time |
| Pouch wrinkles under lid | Film is too flexible or the flange is not matched to the pouch | Adjust lid design, film tension, and application position |
| Moisture loss occurs | Opening seal, film barrier, or lid closure is incomplete | Run leak testing and inspect the inner seal system |
9. How Overseas Buyers Can Specify a Wholesale Lid
When requesting a quotation, send more than a lid photo. Give the supplier the film type, film thickness, film structure, opening diameter, lid color, adhesive requirement, pouch size, wet wipe formula, and expected monthly volume.
Also state the required storage and shipping conditions. A product shipped in a refrigerated container may face different stresses from one shipped through a hot inland warehouse. The lid supplier needs this information to recommend the correct plastic material and attachment system.
A useful buyer specification checklist
- Film: PE, PET, or complete laminate structure.
- Thickness: total thickness and outer layer thickness.
- Surface: treated, printed, coated, or uncoated.
- Lid size: flange width, opening size, and hinge position.
- Application: manual, semi-automatic, or automatic.
- Performance: peel force, resealing cycles, and leak control.
- Environment: temperature, humidity, transport route, and shelf life.
- Order details: sample quantity, monthly demand, packaging, and delivery terms.
10. Final Recommendation for Plastic Wet Wipes Lid Wholesale
For the easiest development path, start with PET or a laminate with a stable PET outer surface. For flexible and cost-sensitive packs, treated PE can provide good performance when the adhesive and lid flange are correctly matched. For barrier packaging, approve the complete laminated structure rather than relying on the word laminate.
The most reliable decision comes from testing the complete package. Compare initial peel strength, aged peel strength, opening force, resealing performance, film appearance, and moisture retention. A minimum 24-hour test is useful, while longer aging gives better protection against transport and shelf-life problems.
Dongyang can help overseas buyers and distributors review wet wipes lid dimensions, plastic materials, adhesive options, and sample testing requirements. The right lid is not simply the one with the lowest unit price. It is the one that remains secure, opens easily, reseals well, and performs consistently on the buyer's real PE, PET, or laminated packaging film.